 繁体中文
 English
 VietNam
 Русский
 日本語

Persistent part defects and creeping cycle times are among the costliest daily challenges for injection molding operations. Many teams spend hours tuning process parameters, switching resin grades, or inspecting mechanical wear — yet overlook the root cause hidden inside the mold: mineral scale buildup in cooling channels. Industry analysis shows cooling system issues account for up to 35% of common injection molding defects, and scale is the single largest hidden driver of extended production cycles.
The Hidden Impact of Scale Buildup
Cooling makes up 60–80% of the total injection molding cycle, making it critical to both production speed and dimensional accuracy. Scale forms gradually inside closed channel walls as dissolved calcium and magnesium minerals precipitate under repeated thermal cycles. Just 1mm of scale reduces thermal conductivity by 7–10%, and a 3mm layer cuts heat transfer by over 20%.
This degraded cooling performance causes three core problems:
- Longer cycle times: Extended cooling periods are required to reach safe ejection temperature, wasting machine capacity and reducing daily output.
- Recurring quality defects: Uneven cooling creates cavity hot spots, leading to warpage, sink marks, dimensional drift and surface blemishes — often resulting in full batch scrap for precision parts.
- Hidden mold damage: Trapped moisture under scale triggers under-deposit corrosion, causing pitting, leaks and permanent tool damage that spurs unplanned downtime.
Why Traditional Cleaning Methods Fall Short
Conventional approaches deliver only temporary relief and fail to break the cycle of recurring buildup:
- Chemical soaking requires full mold teardown, takes 2–3 days of downtime, risks corrosive damage to precision surfaces, and generates hazardous waste.
- Manual rodding/brushing only reaches roughly 60% of channel surface area in complex tooling. Leftover scale acts as a “seed layer” that accelerates re-clogging, forcing shorter and shorter cleaning intervals.
Pulsed Hydraulic Cleaning: A Proven Solution
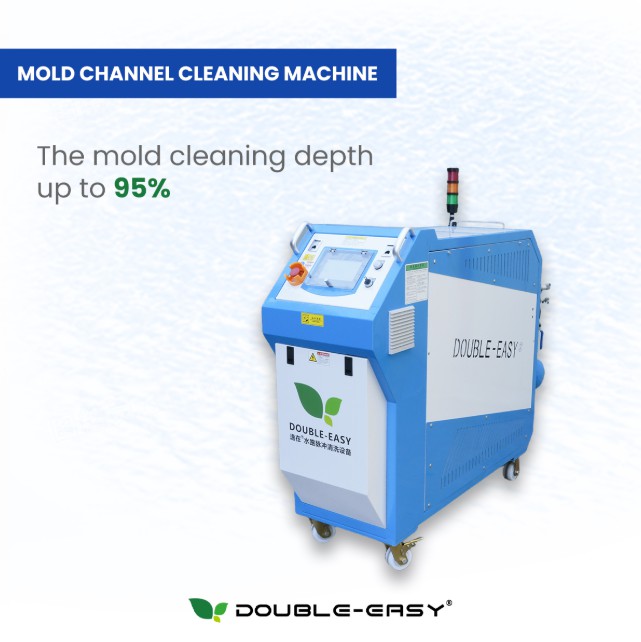
The DOUBLE EASY Mold Cooling Channel Cleaning Machine uses field-proven pulsed hydraulic technology to resolve these limitations. It connects directly to mold ports on the production floor — no teardown required — delivering controlled high-velocity fluid pulses that generate turbulent scrubbing action. This reaches every bend, narrow passage and dead zone to fully remove both soft mineral scale and hard composite rust deposits, without damaging precision channel surfaces or seals.
Its built-in closed-loop filtration system captures debris continuously and recirculates cleaning fluid, eliminating the need for harsh chemicals and cutting water usage by up to 80%. Cleaning time per mold drops from days to hours, and maintenance intervals extend from 3–4 months to 12–18 months with no residual scale to trigger rapid re-clogging.
Recommended Preventive Maintenance Schedule
Align cleaning frequency with operating conditions for best results:
- Light load / softened water: full pulsed cleaning every 12 months, plus quarterly flow checks
- Moderate load / standard municipal water: cleaning every 6–8 months, plus bi-monthly flow verification
- Heavy load / hard water / 24/7 production: cleaning every 3–4 months, plus monthly flow monitoring and inline filtration
Final Takeaway
Cooling channel scale is the most overlooked high-impact factor behind persistent injection molding defects and slow cycles. Upgrading to thorough, non-damaging pulsed cleaning delivers measurable improvements in cycle speed, scrap rates and tool life, with a typical full return on investment within 3–6 months for high-volume operations.




 WhatsApp
